
Handling materials efficiently in industrial and agricultural settings is like keeping a well-oiled machine running smoothly. It’s about ensuring that everything flows seamlessly, from transporting harvested crops to shipping essential goods for manufacturing. Achieving smooth operations involves addressing any capacity issues that might slow things down. This is where Sweetheart™ Elevator Buckets come into play. These specialized buckets are designed to make material handling more efficient, ensuring that every load, whether it’s grain or raw materials, moves safely and easily.
Capacity issues can often disrupt the rhythm of production processes. When materials don’t move efficiently, it can lead to delays and increased costs. The right equipment can significantly reduce such challenges, and Sweetheart™ Elevator Buckets are crafted specifically to tackle these problems. They allow facilities to handle larger volumes of materials without unnecessary interruptions, making them an ideal choice for industries seeking reliable solutions for their material handling needs.
Understanding Capacity Issues in Material Handling
Before diving into solutions, it’s helpful to understand what capacity issues mean in the context of material handling. In both farms and factories, capacity challenges arise when the equipment can’t handle the volume of materials that need moving. This can result in bottlenecks, slowing down processes and affecting overall productivity.
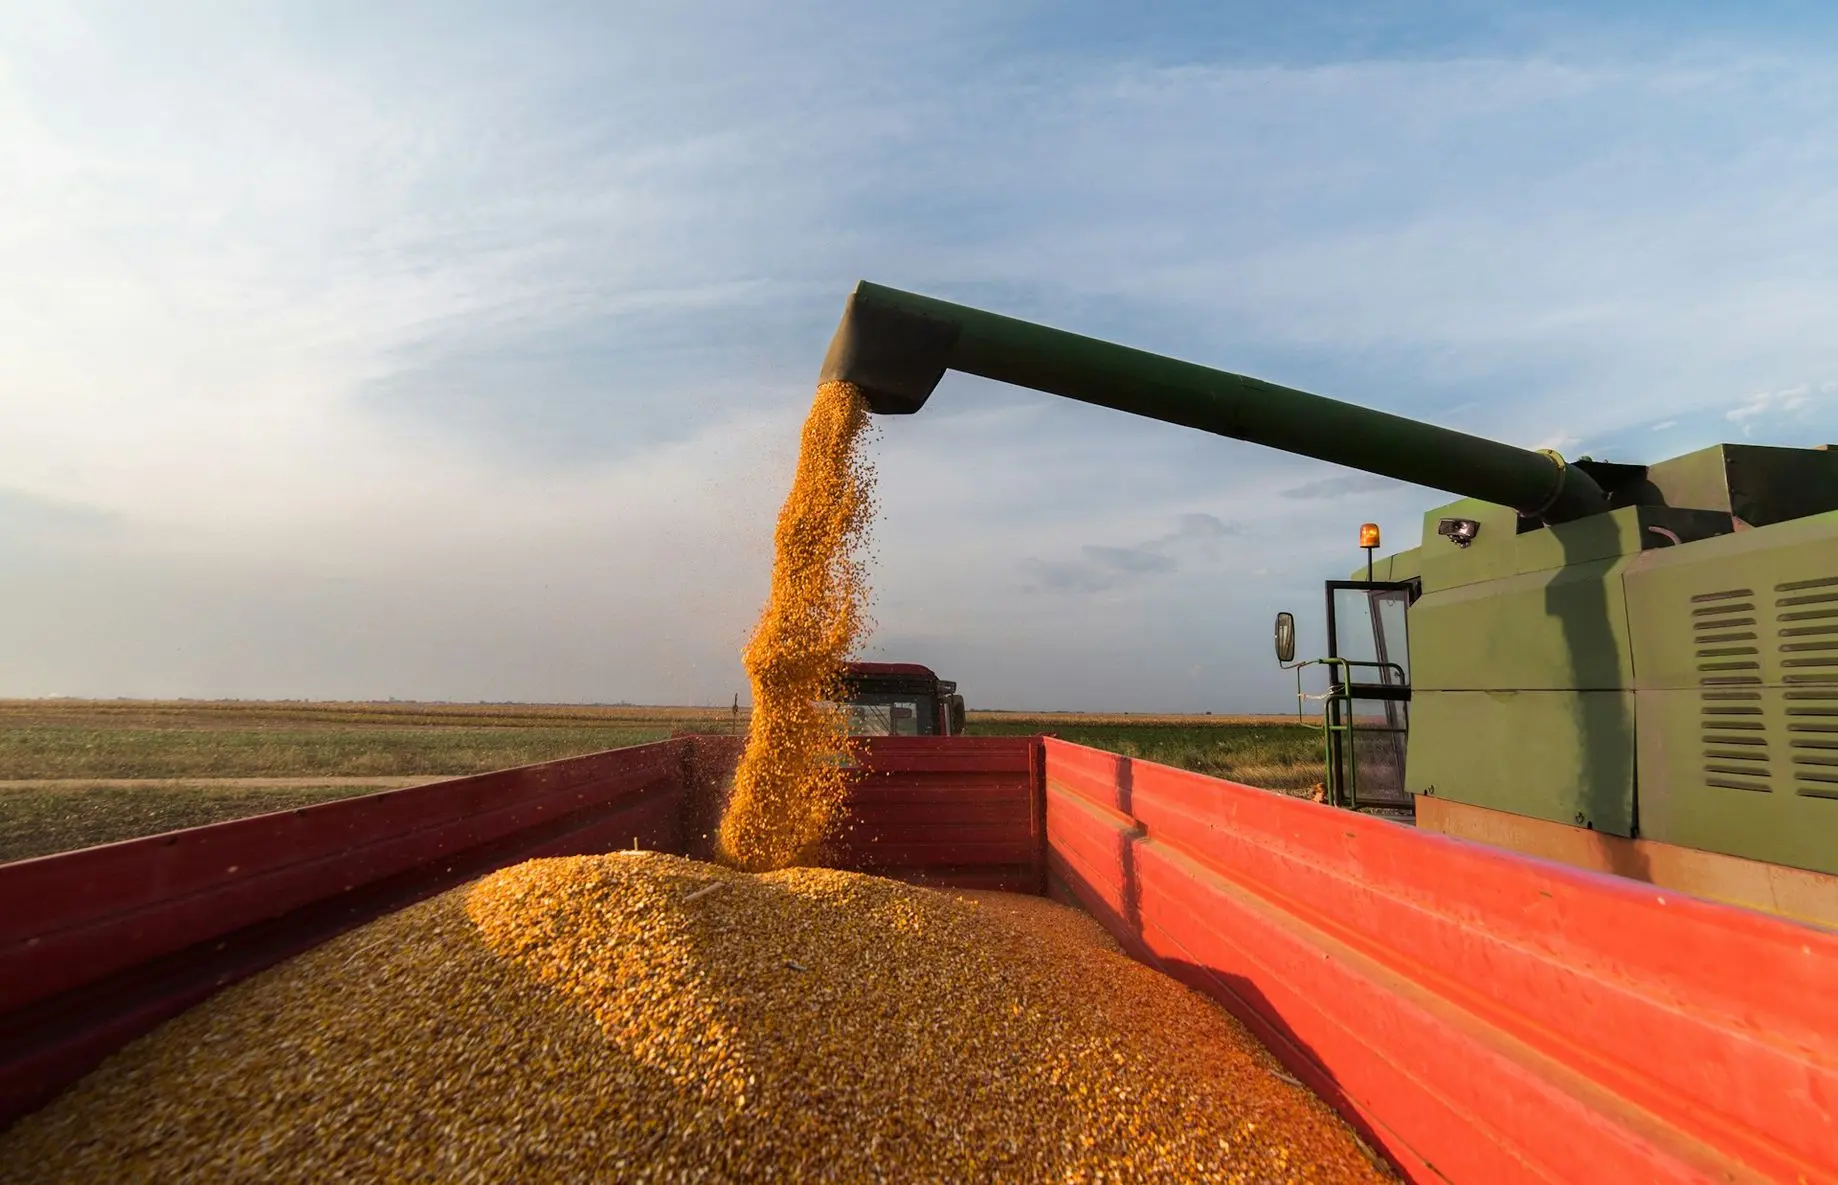
Consider a grain elevator during peak harvest season. If the elevator buckets aren’t operating efficiently, grain transfer slows down. This delay not only affects the harvest schedule but also impacts the storage and quality of the grain. Really maximizing efficiency means using equipment that can handle the load needed without any hiccups along the way.
Capacity issues aren’t just about delays. They can also lead to increased wear and tear on equipment, resulting in more frequent repairs and downtime. This is why it’s crucial to address these problems sooner rather than later. Using the right tools, such as the Sweetheart™ Elevator Buckets, can ensure the equipment functions optimally. When facilities address capacity challenges, they optimize their operations and can manage larger workloads with ease.
Benefits of Using Sweetheart™ Elevator Buckets
When it comes to solving capacity problems, Sweetheart™ Elevator Buckets offer several advantages worth mentioning. Their design helps move larger volumes of material more efficiently, which is key in high-demand environments where every minute counts. Here’s how these buckets stand out:
– Durability: Made from high-quality materials, they’re built to last. This minimizes the need for frequent replacements, saving both time and money.
– Low Maintenance: Their construction requires minimal upkeep, freeing up resources for other tasks.
– Improved Efficiency: They facilitate smoother and faster material movement, enhancing the overall efficiency of operations.
Furthermore, their ability to enhance workflow translates directly to cost savings and increased productivity. By reducing downtime and ensuring a consistent flow of materials, businesses can focus on other critical areas knowing that their material handling processes are in good hands. These buckets are ready to tackle the challenges of busy industrial and agricultural environments.
Case Studies and Real-Life Applications
The practical use of Sweetheart™ Elevator Buckets offers a glimpse into how effectively they handle capacity issues. Picture a large grain storage facility in Springfield, Ohio. During peak harvest, they need to move vast amounts of grain quickly and efficiently to maintain quality and meet demand. This is where Sweetheart™ Elevator Buckets step in. By implementing these buckets, the facility experiences fewer delays, smooth load transitions, and less equipment strain, ensuring operations remain steady.
Another scenario might involve a diverse production environment that includes handling various raw materials. Whether in Springfield or other similar settings, Sweetheart™ Elevator Buckets excel in managing different types of materials without hassle. Their design versatility means they adapt to handle everything from dry grains to more challenging materials like crushed rock or sand, streamlining operations regardless of the task. These real-world applications highlight how essential the right equipment is for optimal performance.
Tips for Optimizing the Use of Sweetheart™ Elevator Buckets
Utilizing these buckets to their full potential involves a few key strategies. First, ensure regular maintenance checks. This not only prevents unexpected breakdowns but also extends the life of the buckets. Scheduled inspections should focus on wear and tear and any debris build-up that might impede performance.
Here’s a handy list for maximizing bucket efficiency:
– Frequent Inspections: Regularly examine the buckets for any damage or wear signs.
– Proper Installation: Ensure buckets are installed correctly in the system to avoid misalignments.
– Routine Cleaning: Clean buckets periodically to prevent material residue build-up.
– Adjust to Load Needs: Adjust the system to match the current load requirements, which minimizes stress on the equipment.
Throughout the process, it’s important to involve experienced personnel or consult reliable resources. Setup accuracy is key in optimizing the buckets’ use, so having a skilled team make necessary adjustments can make a difference.
Keep Your Material Handling Smooth
Addressing capacity challenges through the use of Sweetheart™ Elevator Buckets has proven effective in many situations. Their robust construction, coupled with strategic use, improves facility efficiency, reduces operational headaches, and ensures smoother processing. When handling hefty tasks is a regular part of operations, having dependable tools is like having a trusted friend along for the ride.
These buckets are crafted for reliability and efficiency, making them a smart choice for anyone dealing with substantial material handling tasks. Whether it’s improving transport speed or lessening downtime, these specialized tools help achieve goals efficiently. With their track record, businesses can look forward to enhanced performance and peace of mind throughout their processes.
Boost your facility’s efficiency with Sweetheart™ Elevator Buckets from Sweet Manufacturing Company, engineered to tackle capacity issues with ease. These buckets are integral for businesses aiming to enhance material handling processes, reducing downtime and maintenance needs. Trust in our expertise as a leading bucket elevator manufacturer to deliver high-performance solutions that keep operations running smoothly. Elevate your productivity and handle substantial workloads more effectively today!